

Every core in the shipment can pass while the production process is moving toward a problem.
Acceptance and stability are different questions.
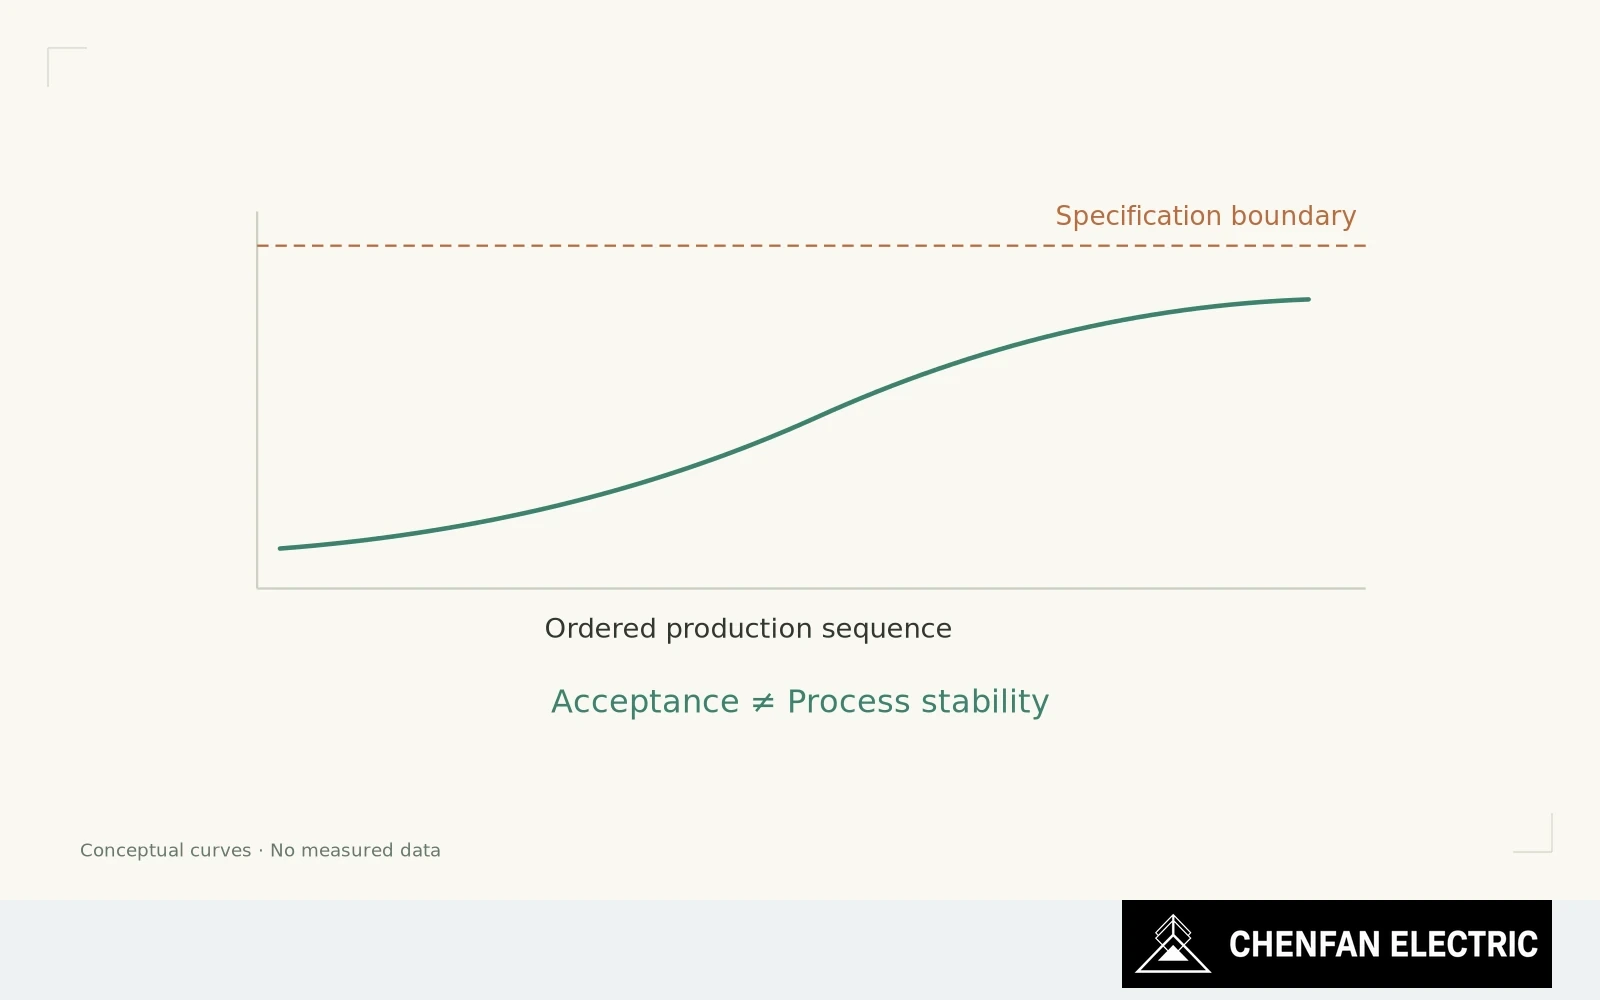
Separate specification limits from monitoring signals
An acceptance limit decides whether a measured unit satisfies the agreed requirement. A process-monitoring method asks whether the pattern of results is consistent with the established process or suggests a change that needs investigation.
For comparable cores, a sequence drifting toward the limit may deserve attention before a failure occurs. Conversely, a single unusual measurement may originate in the test process rather than in the product. The response should discriminate between those possibilities.
Do not use specification limits as though they were statistical control limits. The former come from the required function or agreement; the latter are derived under a particular monitoring method and assumptions. Their purposes differ even when both appear as horizontal lines on a chart.
Retain retests and connect data to action
Keep the production record complete. Repeating measurements until a favorable result appears and retaining only that result removes the very evidence needed to understand variation. A justified retest should preserve the earlier reading and explain the reason for the repeat.
Process controls should be connected to the plausible mechanisms: material identification, cutting condition, sequence integrity, seating and the defined clamping state. Collecting more data is not automatically useful if nobody knows which action follows a relevant signal.
The response plan matters as much as the chart. Who contains potentially affected work? What is rechecked? Which changes require engineering approval? When is normal production released again? These decisions should not depend on the pressure of the particular shipment.
Control the route before final acceptance becomes the alarm
For low-volume core families, a formal statistical chart may not yet be justified. A disciplined time-ordered record and explicit change log can still reveal more than a collection of pass certificates. Avoid forcing unlike designs into one population merely to obtain enough points.
Final testing remains necessary where agreed. Process control supplies a different protection: keeping the route capable of producing the required core without relying on selection and repeated correction at the end.
A supplier’s control system is working when it detects a meaningful change, investigates it and restores a defined condition before the acceptance boundary becomes the only alarm left.
Practical takeaway
A passing shipment can coexist with a deteriorating process trend.
Chenfan Electric manufactures custom transformer cores according to customer drawings. Where applicable to the specified material and core design, agreed process controls include burr height below 0.02 mm and stacking factor above 97%. Measurement methods and acceptance conditions are defined for each order.