

The core passes its magnetic test.
The winding still will not enter the assembly as planned.
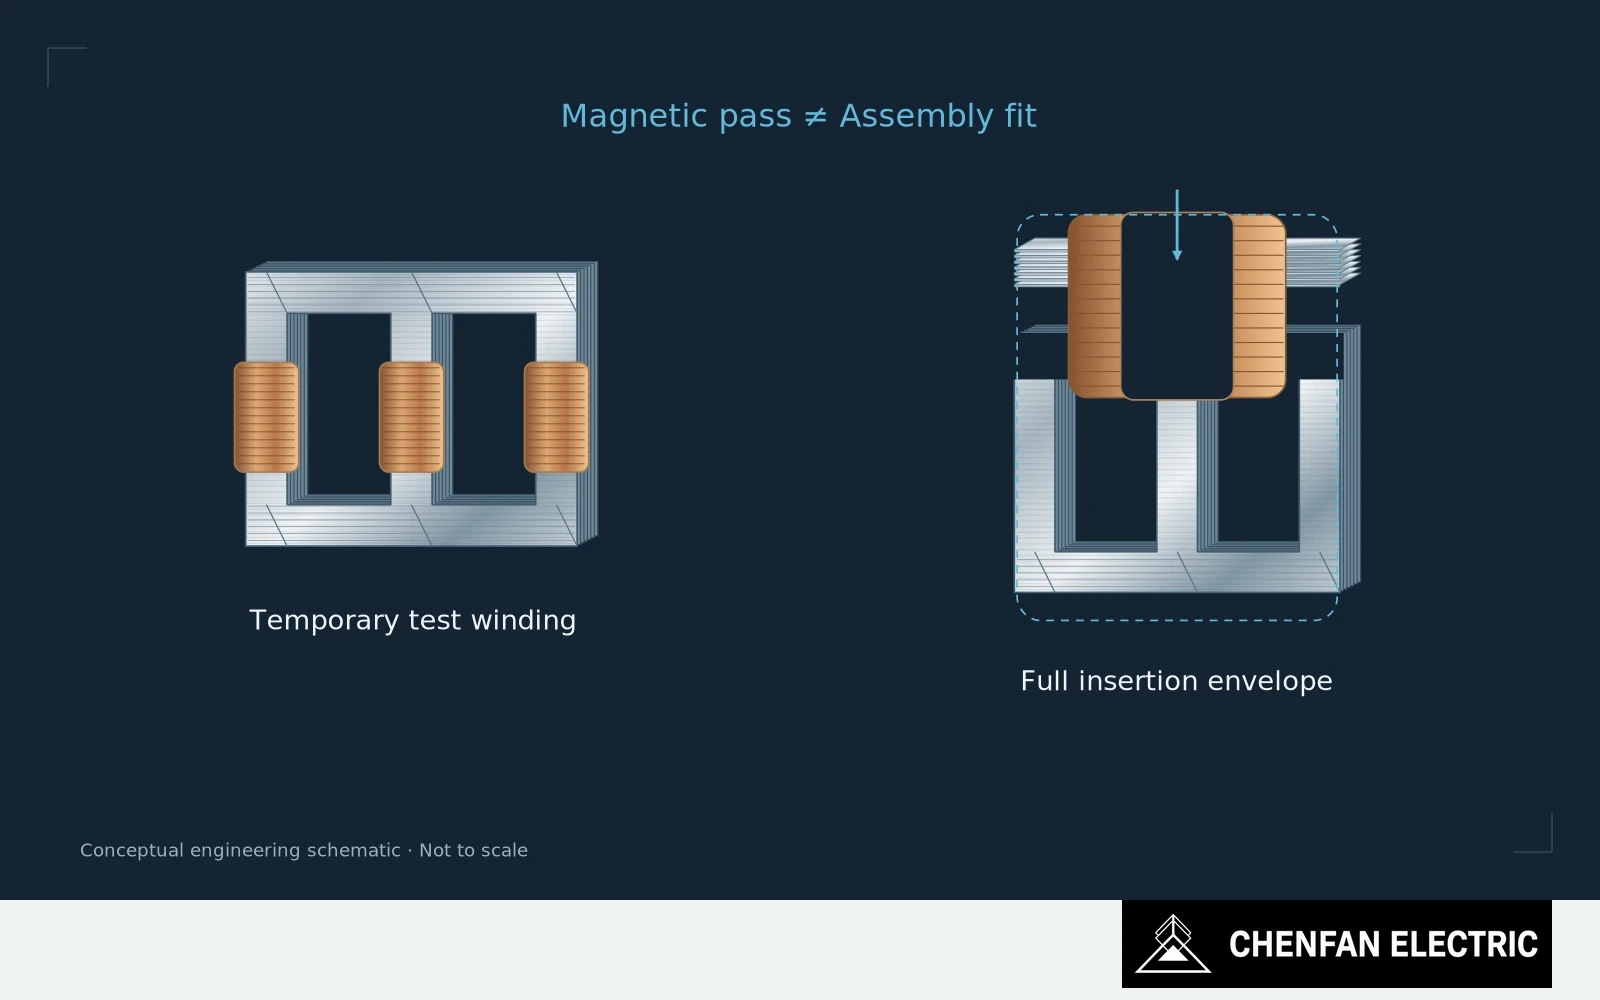
Define the complete winding insertion path
That is a plausible interface failure, not proof that the magnetic test was meaningless.
A temporary test winding can excite a core without reproducing the mechanical path required by the final winding. Electrical acceptance therefore cannot establish coil fit, insertion clearance or the compatibility of the complete clamping arrangement.
The interface begins with more than nominal window width and height. Consider limb envelope, packet projections, winding insulation, lead exits, assembly tools and the path through which the winding must move. The limiting clearance can occur during insertion rather than in the final seated position.
Agree core, coil and clamp interfaces
The datum system matters as well. A core supplier and a winding supplier may each inspect to their own valid reference while the assembled parts require a shared relationship. Separate compliant dimensions do not automatically establish that relationship.
Review the sequence before release. Which parts are fitted before the winding is inserted? Which are removed and rebuilt? Are the measurement states consistent with that sequence? A drawing of the final transformer cannot, by itself, prove that every intermediate assembly step is possible.
This is where a joint interface review earns its time. Core, winding and final-assembly teams should agree the critical envelope and reference features. The supplier need not receive every proprietary winding detail, but must receive enough information to control the interfaces it is responsible for.
Verification can range from a coordinated dimensional study to appropriate gauges or a representative fit check. The method should reflect the actual risk and production scale. A gauge is only useful if its own geometry represents the intended clearance condition.
Verify assembly readiness separately from electrical acceptance
When an interference occurs, preserve the as-found dimensions before forcing or modifying parts. Uncontrolled adjustment can remove the evidence and introduce a new stress or insulation problem.
The commercial acceptance record should distinguish a magnetically accepted core from an assembly-ready core. The latter requires the agreed mechanical interfaces as well as the electrical result.
For a complete assembled-core purchase, ask what has been demonstrated about the winding installation path. “It passed the loss test” answers an important question, but not that one.
Practical takeaway
Electrical acceptance does not reproduce the mechanical path of the final winding.
Chenfan Electric manufactures custom transformer cores according to customer drawings. Where applicable to the specified material and core design, agreed process controls include burr height below 0.02 mm and stacking factor above 97%. Measurement methods and acceptance conditions are defined for each order.