

An offset lamination is not just an untidy edge.
Its significance depends on where the offset enters the joint and the winding interface.
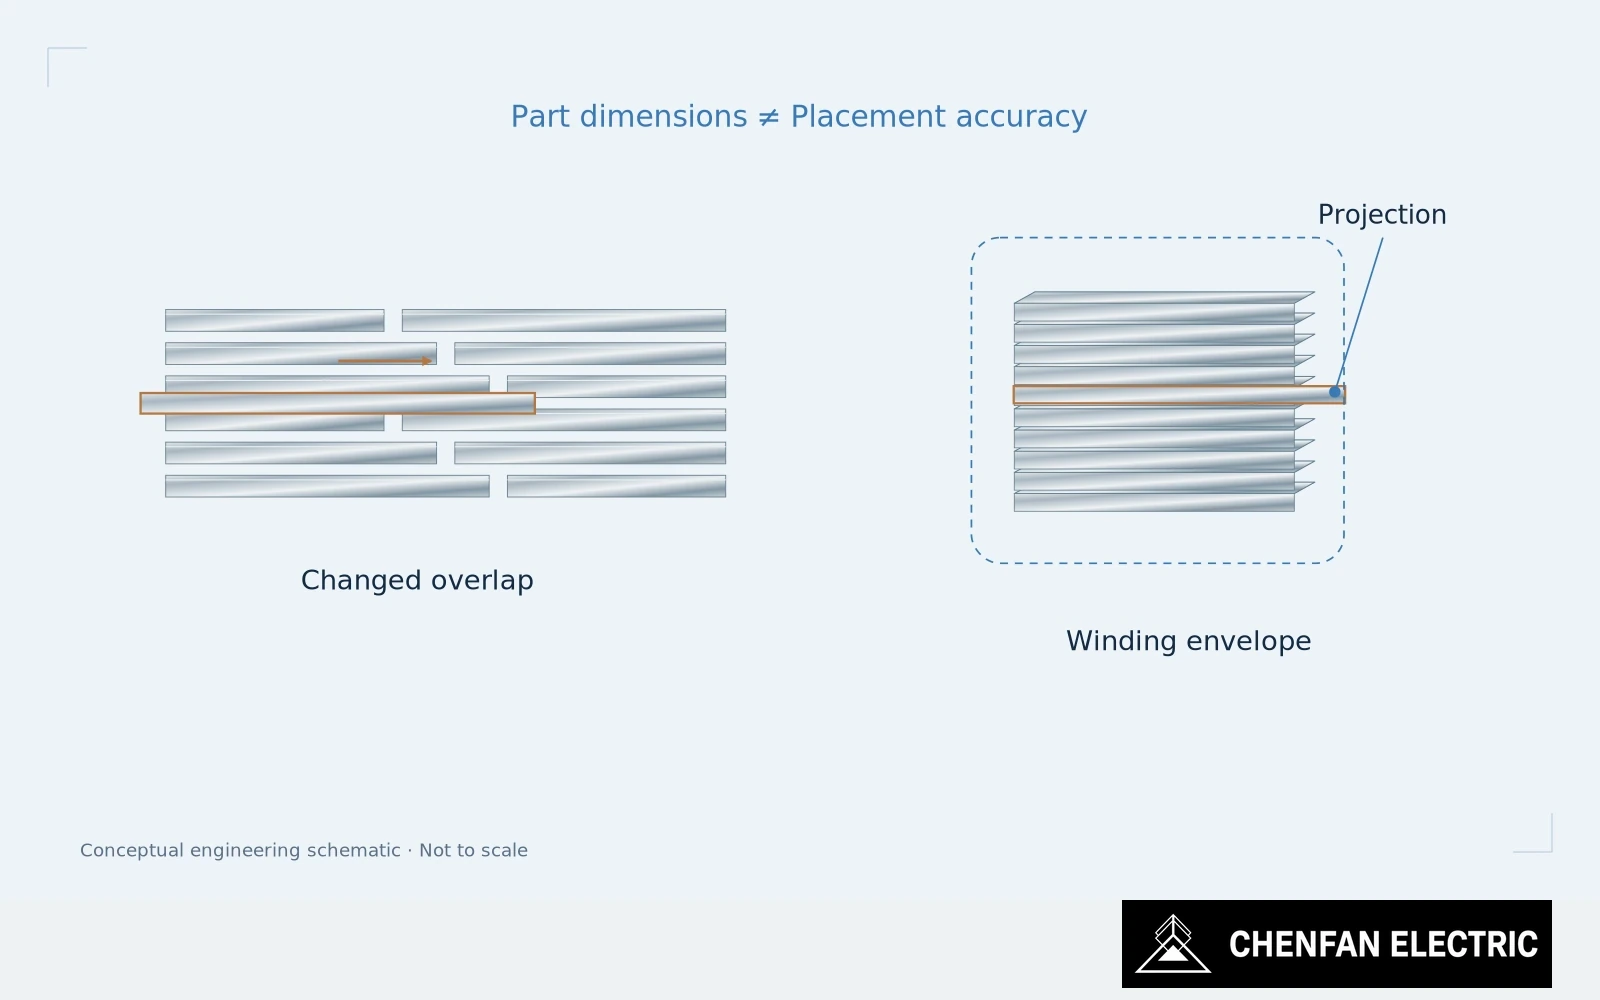
Separate part accuracy from placement accuracy
A sheet can meet its individual length and width tolerances while being positioned incorrectly in the packet. The resulting assembly error is therefore not necessarily a cutting error. It may originate in datum selection, packet transfer or the way a stack is restrained during build-up.
At a step-lap joint, displacement changes the overlap and end-clearance relationships intended by the design. Local flux can redistribute around the altered region. This does not mean every small offset produces a measurable rise in total loss; the influence depends on position, extent and operating induction.
At the limb envelope, the same type of displacement can reduce local clearance for winding insertion. An average limb diameter or a measurement at one height can miss a protrusion along the actual insertion path.
Inspect magnetic joints and insertion envelopes
The two consequences require different checks. Joint sequence and overlap need inspection while the relevant layers remain visible. Winding clearance needs a defined envelope and reference datums in the state used for assembly. A final photograph cannot replace either.
Beware of correcting an accumulated offset by shifting the last few layers. The external outline may improve while the internal pattern becomes less consistent. The point of correction is the earliest operation that introduced the displacement, not the last surface on which it becomes visible.
For long laminations, check whether the locating method constrains both position and angular alignment. A small angular departure can produce a larger lateral offset at a distant joint. The appropriate tolerance comes from the functional geometry, not from applying the same linear limit to every sheet length.
Correct the operation that introduced the offset
Automation can help maintain placement, but it does not remove the need to verify the datum and packet recipe. A robot can reproduce an incorrect offset more consistently than an operator.
During supplier approval, ask for a record that connects the cut part, packet position and final interface. That connection helps distinguish a dimensional part problem from an assembly-position problem when the core reaches your factory.
The useful standard is not photographic neatness. It is the intended joint geometry and a clear winding path, both maintained through the qualified assembly and handling sequence.
Practical takeaway
A sheet can be dimensionally correct but incorrectly positioned in the magnetic assembly.
Chenfan Electric manufactures custom transformer cores according to customer drawings. Where applicable to the specified material and core design, agreed process controls include burr height below 0.02 mm and stacking factor above 97%. Measurement methods and acceptance conditions are defined for each order.