

Stainless steel and carbon steel should not be treated as interchangeable paint substrates. Preparation needs to avoid unwanted contamination and produce the surface condition required by the coating system. Stainless corrosion resistance does not make cleaning or adhesion evidence unnecessary. [1]
Identify the stainless grade, weld condition and previous treatment. Record tools, abrasives, cleaning products and handling contact. Material transfer from shared preparation equipment is a source to investigate, not a conclusion to assign without evidence.
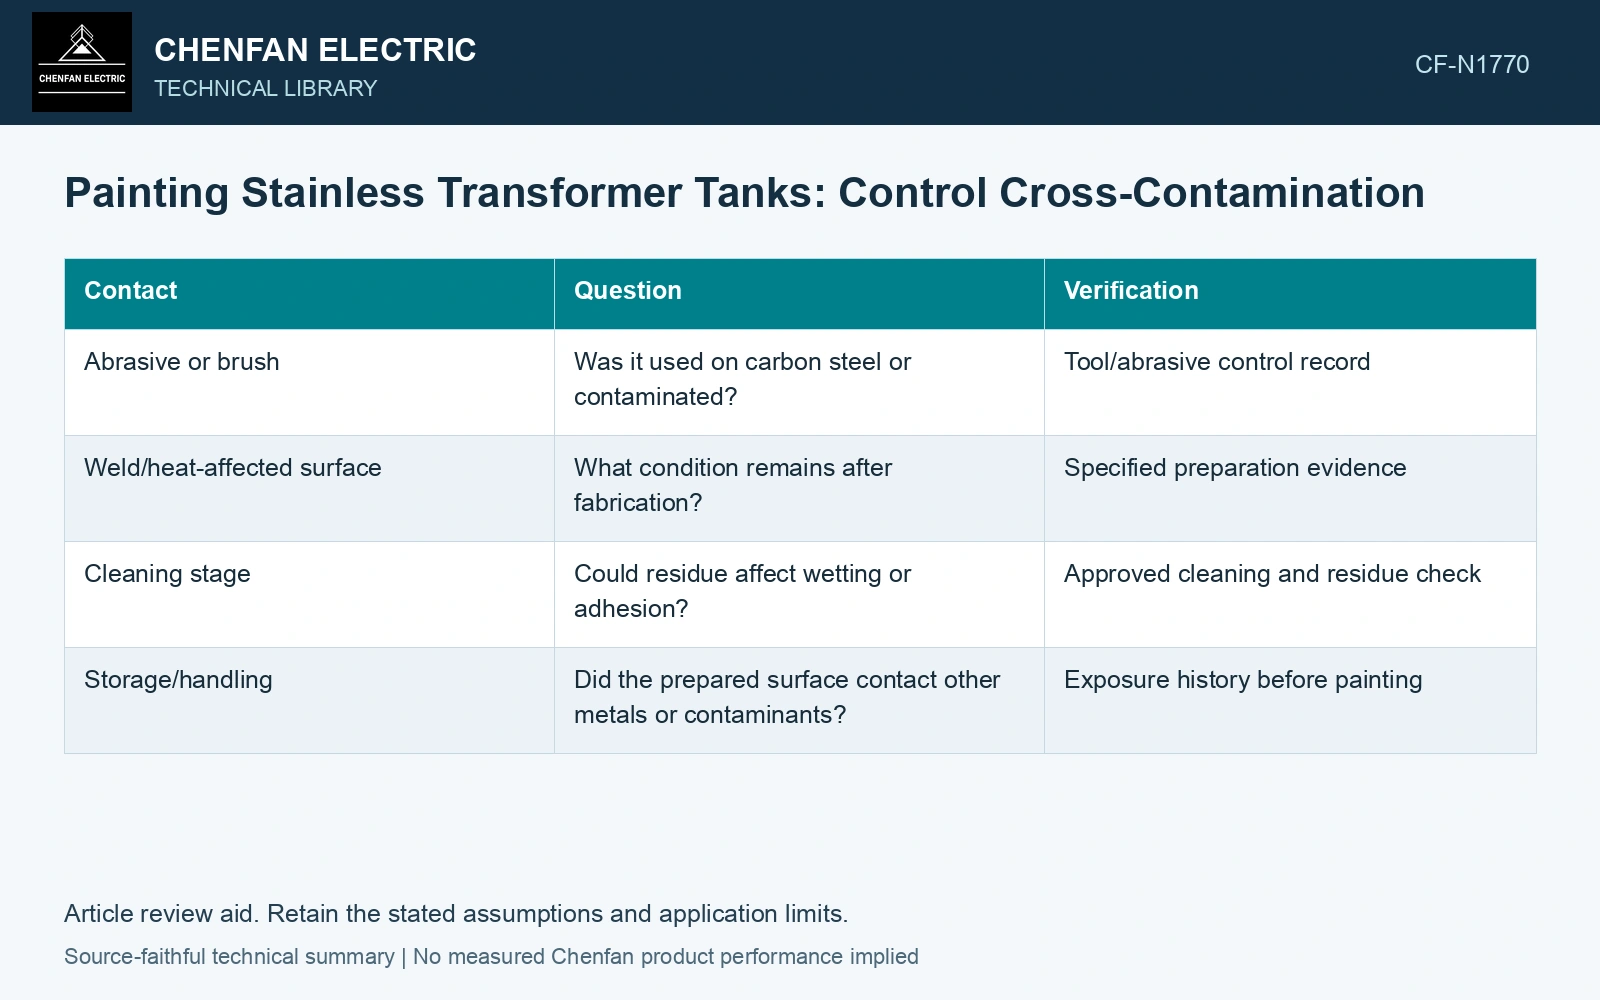
Trace the preparation contacts
| Contact | Question | Verification |
|---|---|---|
| Abrasive or brush | Was it used on carbon steel or contaminated? | Tool/abrasive control record |
| Weld/heat-affected surface | What condition remains after fabrication? | Specified preparation evidence |
| Cleaning stage | Could residue affect wetting or adhesion? | Approved cleaning and residue check |
| Storage/handling | Did the prepared surface contact other metals or contaminants? | Exposure history before painting |
Do not assume one treatment serves every function
A corrosion-oriented surface treatment and a paint-preparation treatment may have different purposes. Verify their compatibility in the approved coating system. A passivation record alone does not establish the roughness or adhesion premise for the next layer.
Conversely, a roughened surface does not prove the absence of contamination. Keep profile, cleanliness and material state as separate inspection entries.
Kotecki and Armao identify contamination from shared tools and fixtures during stainless fabrication and call for stainless-only brushing practice. Carry that contact history into the coating preparation record, then qualify the actual stainless substrate and paint system. [2]
Check qualification coverage for the actual substrate
Assume a qualification file contains six carbon-steel preparation panels and no stainless-steel panels. It provides zero direct stainless-panel results. Resolve substrate-specific preparation, cross-contamination and coating compatibility evidence before extending that file to the stainless tank; the number of carbon-steel tests cannot replace the missing material boundary.
References
- ISO, ISO 12944-4:2017, Paints and varnishes — Corrosion protection of steel structures by protective paint systems — Part 4: Types of surface and surface preparation.
- D. Kotecki and F. Armao, The Lincoln Electric Company, Stainless Steels Welding Guide, 2003, selection of filler metals and joining stainless and other steels.