

A magnetic test report records a condition at a point in the manufacturing route.
Transport adds more conditions. It does not erase the report, and the report does not validate the journey.
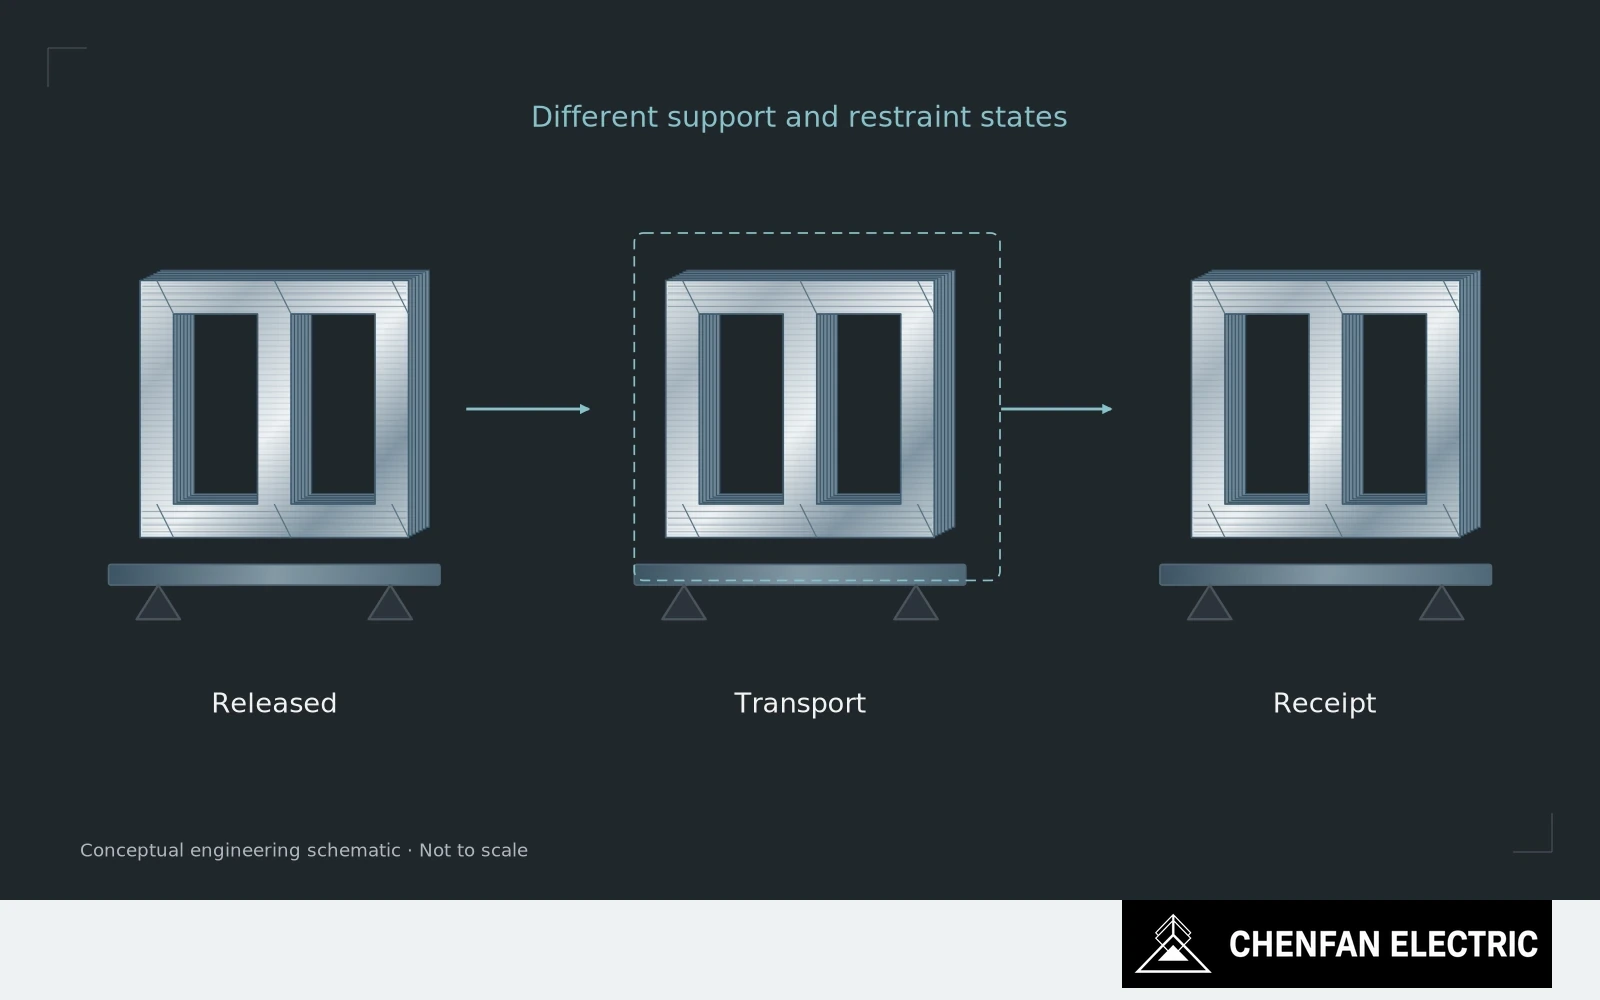
Map the conditions after the factory test
For a complete assembled core, the route can introduce changes in support, restraint, orientation and environment. A port transfer may matter more than the longest section at sea if it changes how the assembly is lifted or supported.
The engineering task is to identify which characteristics must survive each handover. Joint alignment, structural support and protection of lamination surfaces are different objectives. They need different evidence; a sealed package does not prove adequate restraint, and a strong restraint does not prove moisture protection.
Before shipment, retain a baseline that can be used at receipt. Identify the measured datums, clamp and transport configuration, protected surfaces and test state. Photographs should show the relevant reference features rather than only a distant view of the finished package.
Create a useful receiving comparison
At receipt, compare the as-found condition before removing supports or reopening the core. A shock indicator can help identify an event worth investigating, but its trigger alone is not a magnetic failure criterion. Its absence also cannot prove that every internal feature remained unchanged.
Decide in advance which observations trigger further inspection or a magnetic comparison. The decision should reflect the core design, route and available receiving capability. Requiring an identical supplier test at every destination may be impractical; omitting any defined escalation leaves the receiver to improvise.
If a repeat test differs, establish comparable excitation, winding and support conditions before attributing the change to transport. If the buyer has already opened the upper yoke, transport and reassembly are no longer isolated variables.
Connect dispatch, receipt and integration records
This is why the handover record matters commercially. It provides an agreed chronology of the assembly’s condition without assuming that either the supplier or the carrier must be responsible for every later discrepancy.
The aim is not to suggest that transportation normally changes magnetic performance. A suitably engineered and controlled route should preserve the intended assembly. The point is that preservation is an engineering objective supported by evidence, not a property conferred by a pre-shipment certificate.
Treat dispatch, receipt and integration as connected acceptance stages. Then the factory test remains useful when a question appears thousands of kilometres later.
Practical takeaway
A test certificate validates a defined state, not every later transport condition.
Chenfan Electric manufactures custom transformer cores according to customer drawings. Where applicable to the specified material and core design, agreed process controls include burr height below 0.02 mm and stacking factor above 97%. Measurement methods and acceptance conditions are defined for each order.